PPR fitting voids and shrinkage: where we begin
For an injection-moulded fitting, we inspect section thickness, gate position, packing and cooling before proposing a material change. An internal void and a visible sink mark can appear together but may not have the same cause.
Fitting production note
For an injection-moulded fitting, we inspect section thickness, gate position, packing and cooling before proposing a material change. An internal void and a visible sink mark can appear together but may not have the same cause.
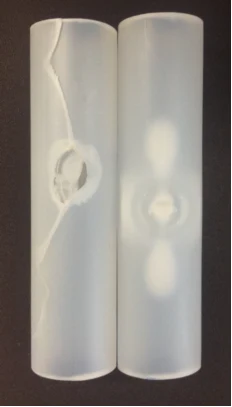
A cut section often tells us more than the outer surface. We compare the location and size of the void, part weight, cycle stages and cavity-to-cavity variation while keeping the resin lot and machine record identifiable.
A useful first sample includes the failed part
Send several affected fittings, one acceptable fitting if available, the resin grade, mould cavity, shot weight and current temperature, pressure and cooling settings. A photograph is helpful, but the physical cross section gives the technical team a better basis for the first trial.